Roto Moulding Machine Factory Capabilities That Drive High-Quality Rotational Molding
2026-10-02
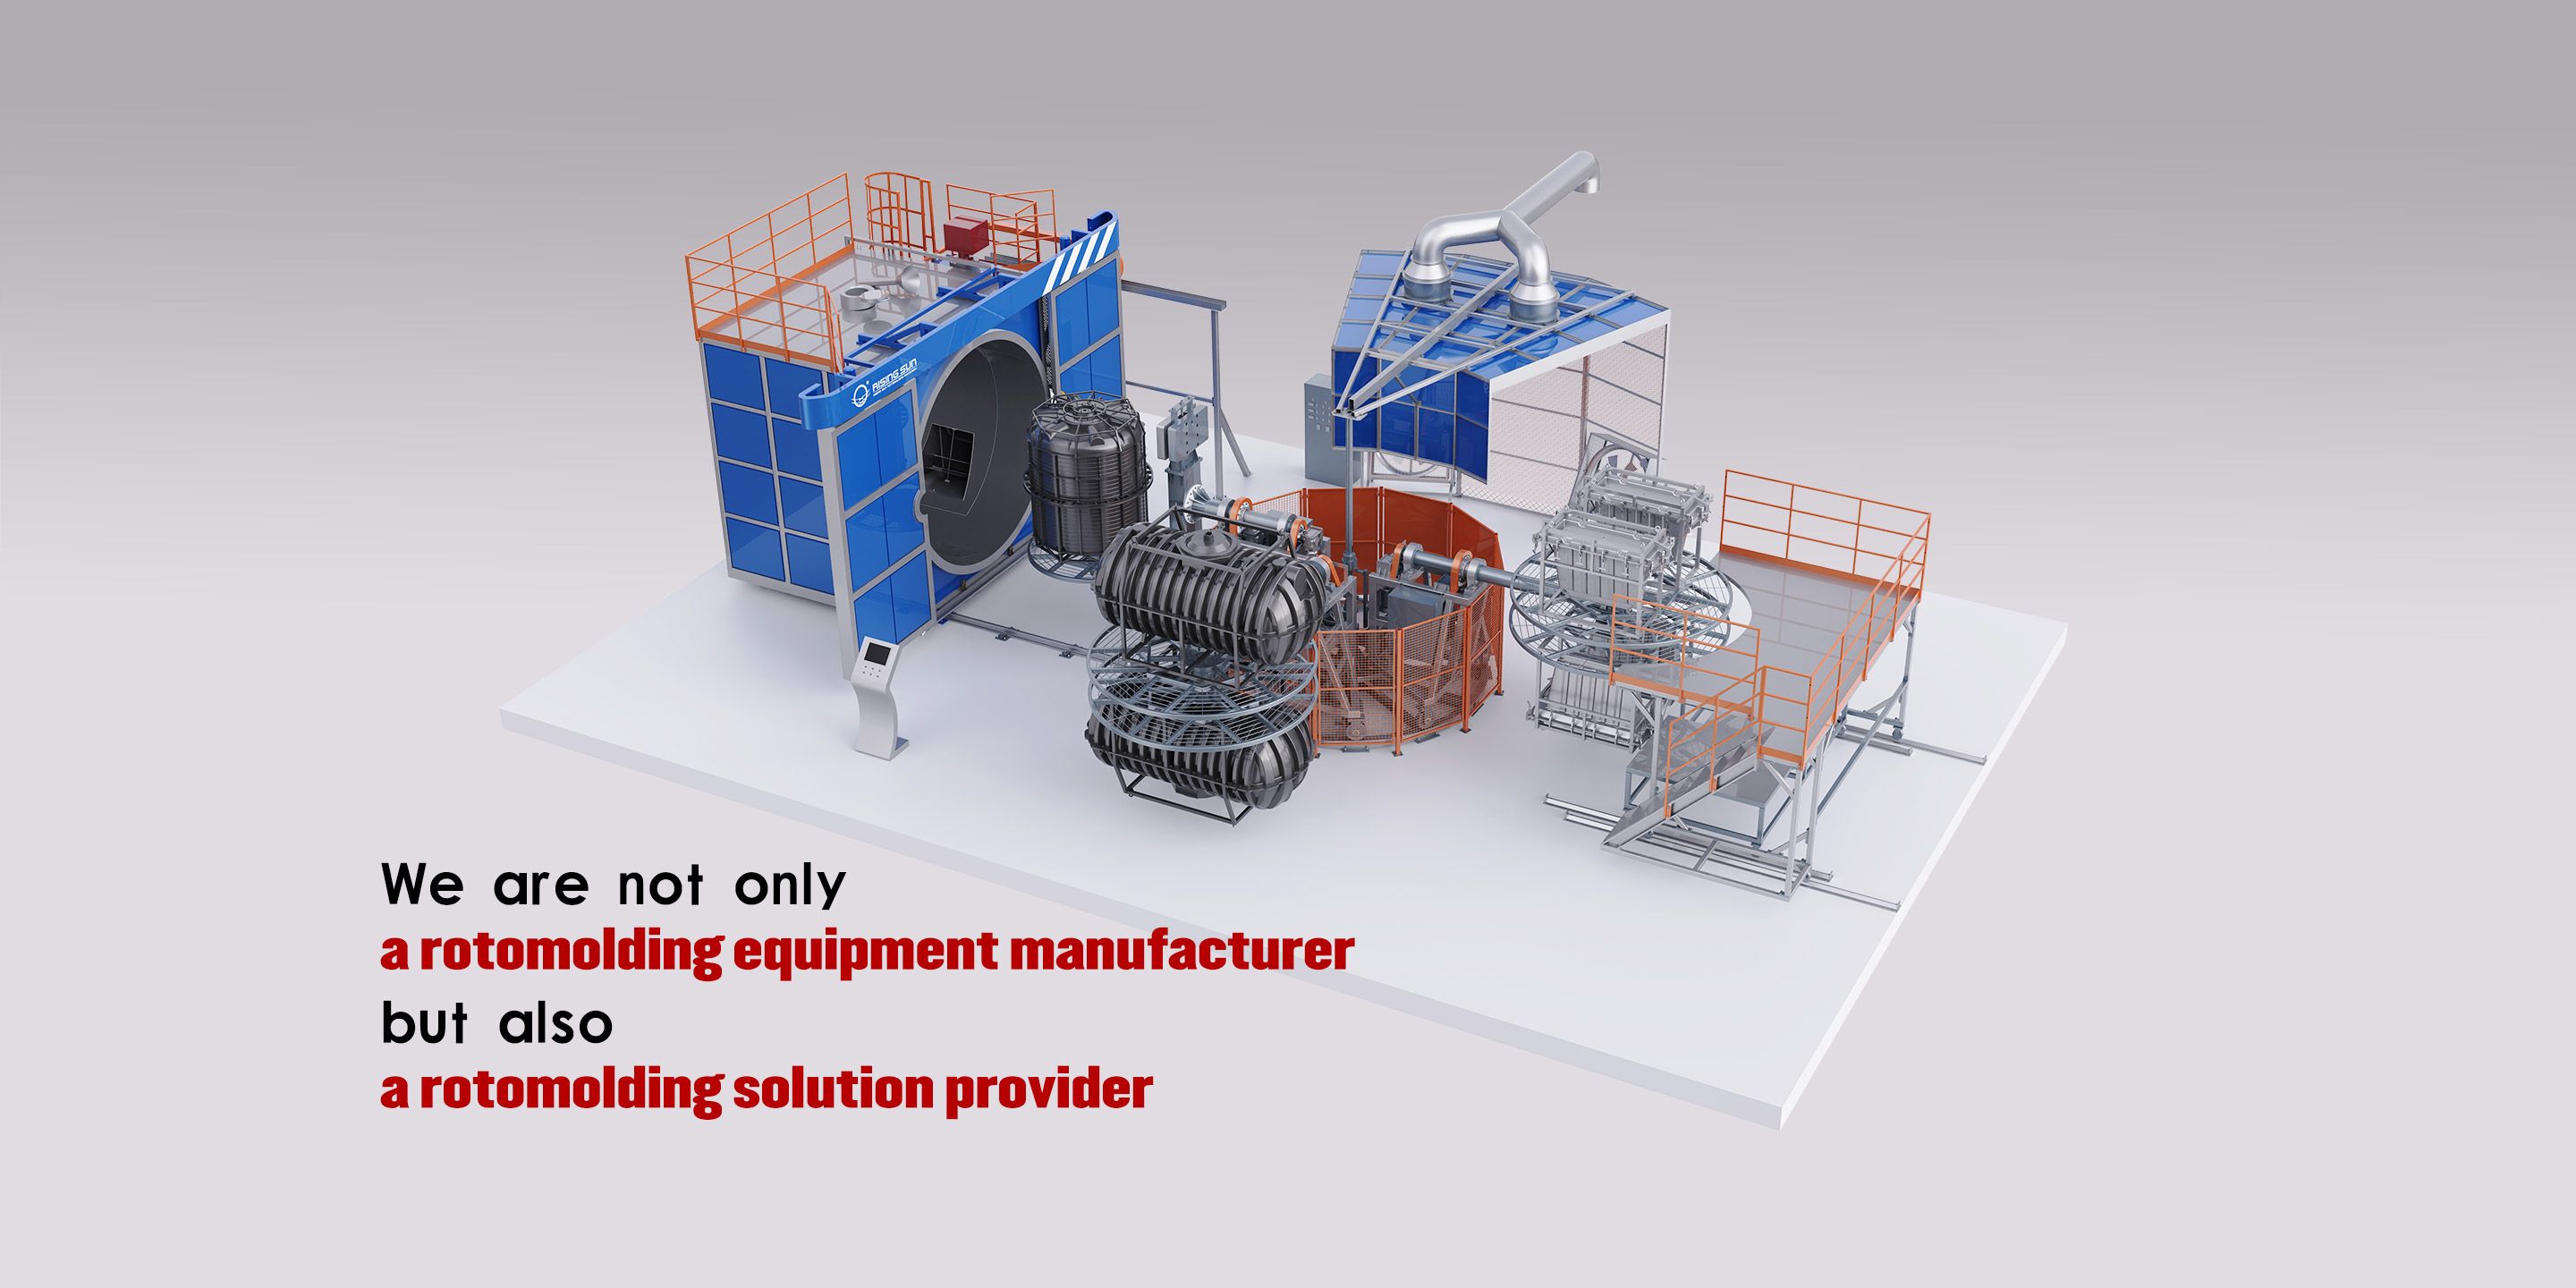
Not every rotational molding machine is built to handle the demands of complex, high-tolerance parts. Behind every flawless tank, kayak, or industrial component lies a factory floor where precision engineering meets raw capability. At Rising Sun, that intersection is more than a promise—it’s a daily reality. From multi-axis robotic arms to oven systems that hold temperature within a single degree, the factory’s capabilities quietly decide whether your next product comes out ready for market or riddled with hidden flaws. In this post, we pull back the curtain on the specific capabilities that set a true roto moulding factory apart—and why they matter more than most buyers realize.
Oven Airflow Mapping That Eliminates Cold Spots
Most ovens don’t struggle because the heating element is weak; they struggle because air gets trapped in lazy pockets around the door, corners, and lower rack. Mapping the airflow means tracking those pockets with a thermal probe or a tray of sugar that browns unevenly. Once you know where the dead zones sit, you can start adjusting fan speed, vent angles, and even the spacing of the rack to push heat through them instead of around them.
A quick way to visualize this at home is to lay parchment over the entire rack, scatter bread cubes in a grid, and run the convection setting for five minutes. The cubes that stay pale mark the cold spots. That map rarely matches what the manual suggests, which is why tweaking the rear baffle or adding a small deflector near the top element can change the pattern more than replacing the element itself.
The goal isn’t perfectly uniform heat—that’s almost impossible in a small cavity—but narrowing the gap between the hottest and coldest zones. In practice, that means fewer rotated trays, less guesswork with multiple racks, and pastries that finish at the same time instead of a burnt edge next to a raw center.
Tooling Built to Handle Aggressive Draft Angles
In moldmaking, aggressive draft angles—often under one degree or even zero—create immediate ejection problems. Standard ejector pins and straight sidewalls don't release cleanly. Tooling has to incorporate custom slides, lifters, or collapsible cores that move along multiple axes at once, pulling the steel away from the part face before ejection force is applied. Harder steels and low-friction coatings like DLC or TiN are common, and cooling lines are routed closer to the steep faces to keep the part from warping as it shrinks onto the core.
A tenth of a degree doesn't sound like much until you multiply it across a tall wall. A 0.5-degree draft on a 100 mm feature exerts serious lateral load on guide components every cycle. Shops counter this by swapping round guide pins for rectangular interlocks or tapered gibs, and by shifting the parting line so the angled surface is not the primary direction of ejection. Hydraulic core pulls are often synchronized with the press opening to retract the steep steel before any push happens.
The most dependable tooling treats aggressive draft as a wear problem, not just a geometry problem. Spring-loaded angled ejectors, rotating cores for internal undercuts, and replaceable wear inserts become standard. Maintenance checklists include a digital protractor reading at every service interval because a few microns of wear on a 0.3-degree face is enough to lock the tool.
Material-Specific Cooling Curves for Dimensional Stability
Cooling rate is rarely uniform across a part, and the resulting thermal gradients dictate how different regions shrink or lock in stress. For semi-crystalline polymers like polypropylene or PEEK, a fast quench suppresses full crystallization, leaving a part that may creep or warp later as slow secondary crystallization proceeds at room temperature. Slower, controlled cooling allows spherulites to develop more completely, improving modulus and reducing post-mold movement, but overdoing it can create excessive shrinkage and sink marks.
Metals show similar sensitivity through phase transformations rather than crystallization alone. In tool steels or aluminum alloys, the path from solutionizing or austenitizing temperatures down to ambient determines whether martensite, bainite, or coarse precipitates form, each with a different specific volume. A material-specific cooling curve therefore maps the temperature-time window that balances transformation completeness, residual stress, and final geometry. This is why a cooling curve optimized for one grade often fails when applied to another, even if the chemistries appear close.
Closed-Loop Process Monitoring With Live Adjustment
A well-tuned controller only works when its view of the process stays accurate. Closed-loop monitoring continuously compares the live sensor stream against the expected behavior, flagging deviations long before they turn into scrap or downtime. Instead of waiting for a batch report or a shift handover, operators see drift the moment it starts, whether that’s a slight pressure rise on a seal, a shifting temperature gradient across a heat exchanger, or a change in vibration signature that never quite matches the baseline. The loop closes when that signal feeds back into the control strategy automatically, nudging setpoints, trimming feed rates, or adjusting cooling flow without someone reaching for a manual override.
Live adjustment makes the system less fragile to raw material variation, ambient temperature swings, and tool wear. Rather than locking every parameter to a fixed recipe, the monitoring layer learns what good output looks like under current conditions and reshapes the operating window accordingly. For example, a packaging line might see film thickness drift slightly after a roll change; closed-loop logic catches the trend and tightens the tension control before seal integrity suffers. In a continuous chemical process, an inline viscosity probe can trigger a solvent trim in near real time, keeping the reactor within the narrow band where yield and quality both hold.
The practical effect shows up in fewer alarms that require human judgment, fewer emergency stops, and a smoother handoff between shifts. Because the system records every adjustment and the evidence behind it, troubleshooting shifts away from guessing which operator changed what and toward reviewing the control timeline. That audit trail also helps engineers recalibrate the underlying model, so the loop gets sharper over weeks and months instead of drifting out of tune. The result is a process that self-corrects quietly, leaving the team free to focus on improvements rather than firefighting.
Rapid Prototype Runs Without Sacrificing Production-Grade Quality
Speed and precision are rarely mentioned in the same breath, but our prototype runs break that assumption. From the first line of code to the final build, every iteration moves at a pace that keeps your team ahead without cutting corners on the underlying architecture. We treat each prototype not as a throwaway draft, but as a foundation that can evolve directly into production. That means no awkward refactors later, no hidden debt waiting to surface.
The difference lies in how we handle the invisible layers. Error handling, logging, security headers, and database indexing are baked in from the very first commit. Many teams push these to the end and then discover their “quick prototype” collapses under real traffic. Here, the prototype already carries the weight of production-grade logic, so when you’re ready to launch, you’re not rebuilding—you’re simply turning the key.
This approach changes the conversation with stakeholders. Instead of saying “we’ll fix it later,” your demos show a system that already behaves like the final product. Users feel the responsiveness, admins see the audit trails, and engineers don’t inherit a mess. Rapid prototyping becomes a true test of the idea, not a gamble on quality.
Post-Mold Trimming and Assembly Handled Internally
Every part that leaves our molding floor passes through an in-house finishing cell where flash, gates, and runners are removed with precision. Rather than shipping unfinished components to an outside vendor, we keep trimming under the same roof, giving our operators direct control over edge quality and dimensional consistency. This eliminates the turnaround delays and miscommunication that often creep in when secondary operations are outsourced.
Assembly is treated as a natural extension of molding, not an afterthought. Our team mates molded halves, presses in inserts, and installs fasteners or clips right at the bench, checking fit and function as they go. Because the same people who ran the mold also handle the build, small issues like a tight boss or slight warpage get caught and corrected immediately instead of turning into costly field failures later.
Keeping trimming and assembly internal also means one accountable partner from raw resin to boxed product. We schedule both steps together, avoid double shipping and handling, and maintain a level of craftsmanship that outside job shops rarely match for low-to-mid volume production. The result is a cleaner part in your hand and fewer surprises on your line.
FAQ
Look for a factory that can run mold filling simulations, adjust heating profiles for challenging geometries, and recommend venting or draft angles before the first prototype is cut. That level of upfront engineering prevents thin corners, internal bubbles, and long trial-and-error runs.
Independent arm rotation speeds, programmable reversal patterns, and multi-station indexing let operators fine-tune how the mold travels through the oven. These settings keep wall thickness uniform from the first part to the five-hundredth, even with complex shapes.
Rotomolding depends on a narrow processing window. A factory that uses multi-zone PID burners and logs temperature data every few seconds can hold the oven within a few degrees of the target. That stability reduces porosity, surface pitting, and premature material degradation.
The best factories will review the mold's thermal mass, add proper vent tubes, and modify draft angles based on the resin and wall thickness you are targeting. Small changes here—like repositioning a vent or adjusting a corner radius—often make the difference between a flat panel and one that bows after cooling.
Servo-driven arms and programmable cycle recipes remove operator variability. Once the heating, cooling, and loading sequence is locked in, every mold sees the same movement and timing. That consistency directly translates to fewer rejects and less manual trimming.
Yes. A factory that offers precision pulverizing, controlled blending of virgin and recycled resins, and moisture monitoring helps maintain consistent particle size and flow. Inconsistent powder can lead to orange peel textures or uneven color distribution on the finished part.
Regular calibration of burners and thermocouples, spare parts stock, and operator training programs are the main ones. Factories that offer remote diagnostics and scheduled preventive maintenance help you avoid drift in cycle times that quietly lowers part quality.
Conclusion
A rotomolding operation only produces consistent parts when the oven truly behaves as designed. Here, airflow mapping goes beyond a routine check—it actively identifies and removes cold spots across the chamber, so every surface of the mold receives the same heat history. That uniformity matters most with complex tooling, especially molds built for aggressive draft angles and deep undercuts. Instead of fighting the process, the tooling is engineered to release cleanly while maintaining wall thickness. Once heating ends, the shift to cooling is just as deliberate. Material-specific cooling curves are applied rather than a generic ramp-down, which keeps shrinkage predictable and dimensional stability intact across runs.
Control doesn't stop at the machine settings. Closed-loop monitoring tracks temperature, rotation speed, and cycle progression in real time, making live adjustments before a drift becomes a defect. That same infrastructure supports rapid prototype runs: short-run molds get the same thermal and cooling discipline as full production, so samples aren't just quick—they're representative. After demolding, trimming and assembly stay in-house, which removes the usual handoff friction and quality gaps. This combination of mapped airflow, purpose-built tooling, tuned cooling, and tight process feedback is what turns standard rotomolding equipment into a reliable source of high-quality parts.
Contact Us
Contact Person: Sharon Zhu
Email: [email protected]
Tel/WhatsApp: 8615712666272
Website: https://www.risingsunroto.com