Filling Machine Manufacturer Guide for Efficient Production Lines
2026-11-16
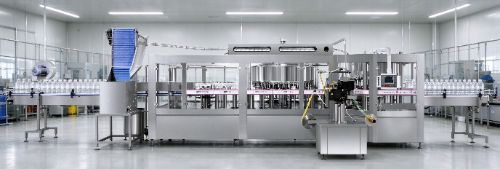
Most filling line bottlenecks aren't caused by the machines you notice—they hide in the choices made before installation. This guide to efficient production lines cuts through the guesswork, showing how the right filling machine manufacturer turns speed, accuracy, and uptime from buzzwords into daily output. Whether you're scaling up or replacing outdated equipment, the principles here—drawn from real floor experience with Wanying Machinery—will help you spot hidden capacity and avoid costly missteps before they reach the line.
Matching Nozzle Design to Your Product's Flow, Not the Other Way Around
Too often, teams start with a nozzle they think looks right, then force the product to behave like it. That approach leads to splatter, uneven coverage, or worse — a dispense line that constantly needs adjustment. A better path is to observe how your material actually moves under pressure, and let that behavior guide the nozzle geometry, orifice size, and internal contour.
Thick, shear-thinning pastes don't respond the same way thin solvents do. A nozzle that works beautifully for a cyanoacrylate will frustrate you with a filled epoxy. Pay attention to your product's viscosity profile, filler content, and any tendency to string or drip. Small changes — like a tapered tip versus a blunt end, or a wider exit angle — can dramatically alter start and stop performance on the line.
The goal isn't to find a universal nozzle. It's to match the flow path so closely that the dispense becomes predictable, even boring. When you achieve that, operators stop fiddling with pressure settings and start trusting the process. The product does what it naturally wants to do; the nozzle simply gives it a clean way out.
Speed Ratings Are a Starting Point, Not a Promise
A tire's speed rating is often mistaken for a green light to push a vehicle to its limit. In reality, the letter stamped on the sidewall—whether it's H, V, or W—reflects a standardized lab test under controlled conditions, not a guarantee that the tire will perform flawlessly at that speed on every road. It's a benchmark, a useful reference point, but it doesn't account for the messy variables of real-world driving.
Load weight, tire pressure, ambient temperature, road surface texture, and even the age of the rubber can dramatically shift how a tire behaves at high speed. A tire rated for 149 mph might handle perfectly on a smooth test drum, yet struggle on a hot highway with a full trunk and underinflated pressure. Treating the speed rating as an absolute promise ignores these everyday factors that can erode a tire's safety margin long before the speedometer reaches the rated figure.
So what should drivers do? Use the speed rating as one piece of the puzzle when selecting tires, not as a license to drive at the upper edge of that rating indefinitely. Check tire condition regularly, keep pressures in line with the vehicle's recommendations, and adjust your speed to match the actual conditions you're facing. The rating is a starting point for making an informed choice—not a promise that the road will always cooperate.
Changeover Time Is Where Efficiency Actually Happens
Most plants treat changeover as a necessary pause between productive runs. That framing quietly hides the real opportunity. When a line stops to switch from one SKU to another, every minute spent on bolts, adjustments, or misplaced tools is a minute the equipment isn't making anything. But the usual fix—pushing people to move faster—rarely sticks. The gains come from separating tasks that require the machine to be down from tasks that can happen while it's still running, then standardizing the remaining work so it doesn't depend on who shows up that shift.
A food packaging line I visited cut changeover from 47 minutes to 11 without buying a single new machine. They moved cleaning steps before the stop, color-coded the change parts, and wrote the sequence on a small laminated card taped near the control panel. Nothing high-tech. What changed was the assumption that changeover time was fixed. Once the team started timing each step and asking “does this really need to happen while the line is down?” the waste became obvious.
What makes changeover time so valuable as a lever is that it compounds. Ten minutes saved per changeover, multiplied by five changeovers a day, across three lines, turns into hours of additional capacity every week. That capacity doesn't require more floor space, more energy, or more labor—just a sharper focus on the transition itself. The most efficient plants aren't the ones that run fastest during steady production; they're the ones that lose the least time between runs.
Building Lines That Adapt to New Formats Without a Full Retool
Traditional packaging lines lock you into fixed dimensions. Change the pouch size, and suddenly you're swapping out forming collars, cutting blades, and sealing jaws—often for hours at a stretch. Smart lines now use servo-driven modules that remember recipes for dozens of formats. Operators call up a new SKU on the touchscreen, and the machine shifts its guides, heat settings, and fill volumes on the fly. That means a single line can run a 50-gram stick pack in the morning and a 500-gram stand-up pouch after lunch, with no hand tools in sight.
The real savings hide in the changeover math. A typical mechanical line might eat up 45 minutes per format switch, adding up to over 100 lost production hours a year for a mid-sized plant. Servo-based systems cut that to under three minutes, sometimes less than 60 seconds. But it's not just speed—it's repeatability. Manual adjustments drift with operator fatigue; encoder-driven axes return to the same position every time, shaving waste from misfeeds and bad seals. One confectionery maker cut film scrap by 18% simply because their new line stopped relying on a technician's "feel" for tension.
There's a quieter benefit too: future-proofing. When marketing dreams up a resealable slider or a shaped gusset, you don't need to rip out the entire forming section. Modular stations click in like building blocks—add a zipper applicator here, swap a heat bar there. The line adapts in hours instead of months. That's how factories keep up with retail trends without betting the capital budget on a brand-new machine every season.
After-Sales Support: The Metric That Predicts Your Uptime
Most companies treat after-sales support as a cost center, but smart operators know it's really the earliest warning system for equipment health. When your support team is fielding the same three complaints week after week, that's not just an annoyance—it's a pattern that will eventually show up as lost production hours. The manufacturers who track this closely can spot a failing component or a weak design before it becomes a full-blown outage. It's the difference between fixing a problem at 2 AM and preventing it from ever happening.
Uptime isn't just about how fast your machines run when everything is working. It's about how quickly you can recover when something breaks, and how well you learn from each failure. A strong after-sales process feeds those lessons back into your maintenance schedules and operator training. If your support team is just resetting passwords or shipping spare parts without asking why the part failed, you're bleeding uptime without realizing it. The best operations treat every support ticket as a data point—not a nuisance to close as fast as possible.
There's a quiet metric buried in your support logs that predicts your next unplanned shutdown better than any sensor on the floor: time-to-resolution with a root cause attached. Teams that resolve issues quickly but never document the underlying cause are running on borrowed time. Teams that take an extra hour to figure out why something broke, and then share that knowledge, see their downtime drop quarter after quarter. If you want to know how reliable your operation will be next month, stop staring at the uptime dashboard and start reading your after-sales reports.
Hygiene by Design: CIP Cycles That Respect Your Production Clock
Conventional CIP scheduling treats sanitation as a pause button—production stops, tanks get washed, and the clock keeps ticking. A hygiene-by-design approach refuses that trade-off. It builds each rinse, caustic wash, and final flush around the actual gaps in your run schedule, so a 40-minute cycle doesn't force a 60-minute idle window. By using inline turbidity sensors to end the pre-rinse the moment it runs clear, or staging drain steps to overlap with the next product's line setup, you recover minutes that used to leak away between batches.
The real leverage comes from mapping your production clock before writing a single CIP recipe. If a filler pauses for 12 minutes during label changes, that's your window for a targeted acid pass on the downstream pipework. Swing connections or double-seat valves let one circuit finish its final rinse while the adjacent circuit starts its pre-rinse, so the cleaning skid never becomes the bottleneck. Validation stays intact because each abbreviated phase is tied to a measurable endpoint—conductivity, temperature, flow rate—not just a stopwatch.
Plants that adopt this mindset see fewer sanitation-related delays and less water heated for no reason. The goal isn't simply faster cleaning; it's cleaning that obeys the line's natural rhythm. When a short product run leaves only 22 minutes before the next start-up, a risk-based CIP design knows exactly which surfaces need aggressive chemical action and which only need a hot water push. That kind of precision keeps the production clock running with fewer interruptions—and without gambling on microbial safety.
FAQ
Look beyond the spec sheet. Ask about changeover times between bottle sizes, whether their servo-driven fillers maintain accuracy at top speed, and if they can provide a documented track record in your specific container type. A manufacturer that asks about your product viscosity, carbonation level, and line layout before quoting is usually worth shortlisting.
The quickest wins come from reducing micro-stops. Modern fillers with automatic nozzle positioning and no-container/no-fill sensors cut down on splashing and rejected units. Pair that with recipe-driven changeovers under ten minutes, and your availability jumps without adding extra staff.
Focus on the fill zone. Daily cleaning cycles with CIP-compatible designs prevent product buildup that causes drips and inaccurate fills. Weekly checks on seal wear and pneumatic pressure, plus monthly calibration of load cells or flow meters, will catch drift before it hits your fill weight variance limits.
Usually yes, if your volume justifies it. Standard piston fillers struggle with particulates and air pockets. Look for manufacturers offering positive displacement pumps with gentle product handling and hopper agitation. Custom nozzles that retract during fill reduce stringing and give you cleaner container rims, which lowers rework downstream.
Automation shines in inspection and data logging, not just motion. Inline weight checkers with feedback to the filler and vision systems for cap placement pay back fast. But avoid automating every manual task; a semi-automatic load station for empty containers may cost less and break down less than a fully robotic cell if your operators are already nearby.
Get itemized quotes that separate wear parts, recommended spare kits, and service travel rates. Ask for utility consumption figures—air and electricity—at your target output. Then talk to at least one reference running the same product family. A slightly higher upfront price often disappears after two years of lower rejects and faster support response.
Request a clear response-time SLA for remote diagnostics and on-site visits. Ask if the manufacturer stocks critical components locally or ships from overseas. Verify whether they offer operator training at your facility and if their software updates are included for the first year. The best vendors will share a spare parts list tied to your runtime hours.
Conclusion
A filling line only performs as well as its least considered component. Start with nozzle selection: a design that fights your product's viscosity, particulate size, or foaming tendency will cap your throughput no matter how fast the machine cycles. Treat the manufacturer's speed rating as a laboratory benchmark, not a guarantee you can hit with your actual formulation and container. The real gain often hides in changeover. Lines that let operators swap formats, clean contact parts, and reset parameters in minutes rather than hours turn batch production into continuous output. Plan for future SKUs by choosing modular conveyors, quick-release guide rails, and tool-less adjustments, so a new bottle shape or cap style doesn't trigger a full retooling project.
Uptime is purchased after installation. Evaluate a supplier's spare parts availability, remote diagnostics, and technician response times as rigorously as you evaluate their machinery. A filling line that can't be serviced quickly will idle, and idle time is never recovered. Hygiene should work with your production clock, not against it. Look for CIP systems that clean in place without requiring full disassembly, with cycle times short enough to fit between scheduled runs. Drainability, sloped surfaces, and sealed cabinets cut contamination risk and reduce the labor hours lost to manual sanitation. The best filling machine manufacturer is not the one with the highest spec sheet, but the one whose equipment matches your product behavior, supports fast changeovers, adapts to new formats, and stays running because service and cleaning are built into the design.
Contact Us
Contact Person: Tyson
Email: [email protected]
Tel/WhatsApp: +8613396971296
Website: https://www.wanyingmachinery.com