Double Pitch Sprockets Factory Precision Manufacturing Process Unveiled
2026-10-10
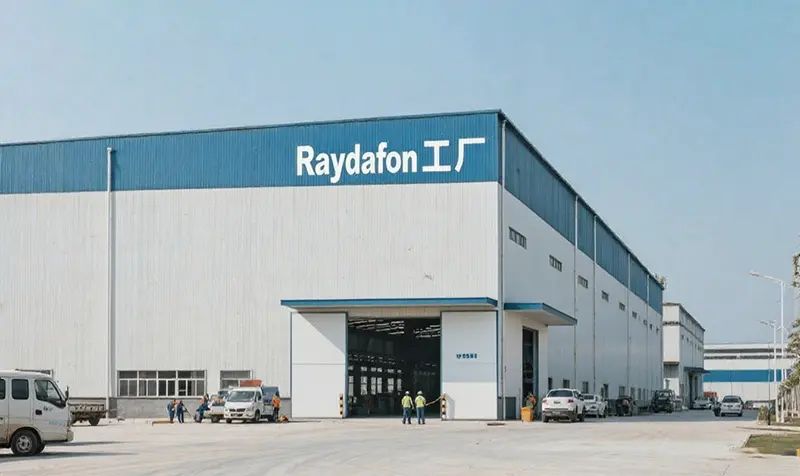
Most people never see inside a double pitch sprocket factory, and even fewer understand what precision really means until they watch a blank get machined into a perfectly spaced tooth profile. At Raydafon, we are pulling back the curtain on our manufacturing floor. From raw bar stock to final inspection, every step is engineered around one thing: keeping your conveyor lines moving without unexpected downtime. Here is what actually happens behind the gates.
Raw Steel That Earns Its Place in a Double Pitch Blank
Raw steel in a double pitch blank isn't just a material choice—it's a statement. The uncoated surface carries the honest marks of its making: faint mill scale, subtle roller lines, and a tactile grain that feels alive under your fingertips. Unlike polished or painted finishes, this steel asks to be noticed for what it is, not what it mimics.
In the context of a double pitch blank, that rawness does real work. The blank's dual-angle geometry already demands attention; pairing it with untreated steel lets the form speak without a glossy distraction. The metal catches light unevenly, shifting from graphite to silver depending on the angle, which makes the blank feel less like a static object and more like a piece of industrial archeology.
This isn't steel that hides behind a coating. It oxidizes slowly in the open air, developing a patina that maps its environment. For makers and collectors tired of perfect, uniform finishes, this raw steel earns its keep by staying imperfect—and by getting better with every scratch, every touch, every year.
Tooth Cutting That Won't Forgive Even a Half Micron
In gear manufacturing, the final tooth profile either locks into place with a near-silent mesh or it reveals every shortcut taken upstream. Here, a half micron isn't a rounding error—it's the difference between a flank that wears evenly over twenty thousand hours and one that starts spalling before the first oil change. The cutting edge doesn't negotiate. If the hob or shaper leaves a trace of drift, the inspection report doesn't soften the language.
What makes this threshold unforgiving is the way micro-deviations stack. A slight thermal shift in the blank, a worn tip on the cutter, a fixture that was true yesterday but off today—each one barely visible alone, yet together they push the involute past the line. Operators who work this tight learn to read the machine's hum, the curl of the chip, the faint pattern left on the surface. They don't chase the tolerance after the cut; they remove the variables before the spindle starts.
The result isn't just accuracy on paper. It's a tooth flank that shares load the way the design intended, keeping noise down and fatigue life predictable. Half a micron is small enough to hide under a fingerprint, but in a gearbox spinning at full load, it might as well be a canyon.
Heat Treat Curves Tuned for Conveyor-Beating Longevity
The cadence of a heat treat curve isn’t just a technical footnote—it’s the difference between a conveyor chain that shrugs off daily abuse and one that surrenders after a few hundred cycles. We’ve pulled back the veil on how subtle shifts in ramp rates and soak timings can harden the wear surfaces without sacrificing the core’s toughness. Instead of relying on a one-size-fits-all profile, our process maps the actual load patterns a conveyor faces: shock loading at transfer points, constant abrasion from fine particulates, and thermal swings that would embrittle a lesser alloy.
Tuning the curve means playing with the austenitizing temperature just enough to dissolve carbides evenly, then dropping into a quenching medium that doesn’t crack the thin cross-sections common in chain links. We’ve found that a stepped aging stage—rather than a single long soak—creates a dispersion of fine precipitates that resists both pitting and fatigue. The result is a surface that stays above 58 HRC while the inner link retains enough ductility to stretch instead of snap when a jam occurs. It’s that balance that lets the conveyor keep running long past the expected maintenance window.
Pitch Inspection Stations Designed to Reject, Not Just Pass
Most ground inspections begin with a nod and a wave, but the stations built to actually protect players work the other way around. They assume from the outset that a surface is unsafe until proven otherwise, and every checkpoint is arranged to force a refusal if the evidence is even slightly ambiguous. That means no rubber-stamping at the end of a long drive, no reasoning that it will probably be fine, and no pressure on the inspector to keep a fixture alive.
A well-designed rejection-first station uses objective tools instead of opinion. A penetrometer reading, a moisture sensor, a stud-test plate for hardness, a simple measured grid for bare patches. Each reading has a hard fail threshold, and one failed box on the sheet is enough to stop the match. The layout also matters: inspectors walk the full pitch in a set pattern, not just the centre circle, because the corner areas and goalmouths are where most injuries happen.
Over time, clubs learn that the station will not bend, so they prepare pitches to meet the standard rather than hoping for a lenient once-over. That is the real purpose. Rejection is not there to punish; it is the only mechanism that makes the pass meaningful.
Assembly Jigs That Catch the Slightest Tooth Misalignment
Gear and spline assemblies used to rely on an operator's feel or a quick visual check to confirm tooth engagement, but a misalignment of just a few hundredths of a millimeter can slip past unnoticed. The latest assembly jigs tackle this by embedding linear encoders and micro load cells directly into the press head, so the moment a tooth starts to bind instead of slide into its mating groove, the force signature shifts. If the real-time torque curve deviates from the expected profile by more than 0.02 N·m, the jig locks the ram, flashes a fault light, and holds the parts in place rather than forcing them together.
On an electric drive unit line, these jigs use a non-contact laser profiler that sweeps the full gear circumference in under half a second. The system overlays the captured tooth positions onto the CAD model and flags a single tooth with 0.008 mm of radial runout, which is enough to cause whine at highway speeds. Unlike older fixtures that only checked total indicated runout after pressing, this approach catches the error before the bearing seats are loaded, letting the operator back the ram off, rotate the gear one tooth, and retry without scrapping a costly rotor shaft.
The real benefit shows up in teardown audits: parts assembled with these jigs consistently measure less than 0.01 mm of tooth-to-tooth spacing error, versus 0.04 mm or more with conventional blind pressing. The jig bodies are machined from stress-relieved aluminum and use quick-change mandrels, so a line can switch from a 21-tooth pinion to a 27-tooth ring gear in about four minutes without recalibrating the load cell range.
Final Audit: Each Double Pitch Sprocket Leaves a Traceable Mark
Before a double pitch sprocket leaves the floor, it gets a permanent identity—typically a laser-etched serial number or a compact data matrix code. This isn't just for inventory. The mark links directly to the sprocket's full production file: the specific heat number of the steel, the CNC machine that cut the teeth, the exact temperature curve from heat treatment, and even the operator who ran the final inspection.
The final audit itself goes beyond a visual once-over. Each sprocket is checked against its drawing for pitch accuracy, bore tolerance, and tooth profile deviation. Those measurements are recorded, not as pass/fail checkmarks, but as actual values tied to the serial number. If a sprocket ever comes back with unusual wear or a dimensional issue, a quick scan of the mark pulls up the entire history—no guesswork, no lost paperwork.
For maintenance teams, that traceability changes how replacements are handled. When a sprocket from a specific batch shows early fatigue, you can identify every other sprocket from that same heat or machine run before they fail. It's a level of accountability that turns a simple metal part into a documented component, and it's the reason some facilities won't accept sprockets without a readable trace code.
FAQ
A double pitch sprocket has teeth spaced at twice the pitch of a standard sprocket, which lets it work with double pitch chains. This design cuts weight and cost while still handling light to moderate loads, commonly found in conveyors and agricultural equipment.
We lean on carbon steels like C45 and 40Cr for most runs, with options for stainless steel or engineered plastics when corrosion resistance or low friction matters. Each batch gets hardness-tested before machining so there are no surprises later.
It starts with laser or plasma cutting the blank, then moves to CNC turning and hobbing to form the tooth profile. After that, we do heat treatment, shot blasting, and a final bore honing. Every step has in-process checks, not just a final inspection.
We use CMM inspection for tooth spacing and runout, plus magnetic particle testing on critical lots. There's also a load test on a sample from each heat lot to confirm the sprocket holds its rated torque without deformation.
After the teeth are cut, we heat treat to around 45-50 HRC. This hardens the tooth surface while keeping the core tough, so the sprocket resists wear and shock loads. A poorly heat-treated sprocket will lose teeth within months, so we monitor furnace temps continuously.
Most go to agricultural machinery, food processing conveyors, and packaging lines. Food-grade applications require smoother finishes and sometimes plastic materials, while agricultural uses need looser tolerances but higher impact strength. We adjust the process accordingly.
We keep a digital record of every machine parameter and tool change. Each sprocket gets a laser-etched lot code, so if there's ever a field issue, we can trace it back to the exact shift and machine. That plus SPC charting on key dimensions keeps variation low.
We don't just sell sprockets; we offer full traceability and can handle custom bore sizes or special hub configurations without long lead times. Our in-house heat treatment and CMM inspection mean you're not relying on a third party for critical quality steps.
Conclusion
The production floor for double pitch sprockets begins long before the first cut. Incoming steel is sorted by its response to blank forming, with suppliers held to a tight chemistry window that predicts how the metal will flow under the press. Blanks that make it through are checked for flatness and density at the rim, because a sprocket that starts slightly off-center will never recover downstream. The tooth cutting stage then removes material in passes calibrated to half-micron tolerances, using cutting tools that are replaced on a wear schedule rather than waiting for visible dulling. Even the coolant temperature is monitored, since a few degrees of drift can shift tooth geometry enough to matter on a long conveyor run.
Heat treatment is not a fixed cycle but a curve tuned to the sprocket's pitch and service load. Operators track case depth and core hardness from furnace charts, rejecting batches that land outside the narrow band. Every sprocket then moves to a pitch inspection station built to reject, not merely pass, parts. Here a mandrel with a known master profile checks tooth spacing across the full circumference, flagging any deviation that could cause chordal action or uneven wear. Assembly jigs add a second layer: each sprocket is mounted and rotated against a reference chain segment, so even a slight tooth misalignment is caught by feeler gauges before it leaves the cell. The final audit stamps a traceable mark—a serial number linked to batch heat numbers, machine settings, and inspector sign-off. That mark travels with the sprocket into the field, giving maintenance teams a direct line back to the exact conditions under which the part was made. It closes the loop between factory precision and conveyor uptime in a way that a generic catalog number never could.
Contact Us
Contact Person: Mr. Shen
Email: [email protected]
Tel/WhatsApp: +86-574-87168065
Website: https://www.transmissions-china.com/