Custom Energy Drink Production Line Solutions for Modern Beverage Brands
2026-10-16
Your energy drink might have a killer formula, but if the production line can't keep up with changing can sizes, carbonation levels, or batch volumes, you're leaving market share on the table. Standard machinery often forces modern beverage brands into awkward compromises. That's why custom energy drink production line solutions matter more than ever. INTOP Machinery builds flexible, turnkey systems designed around your specific product and growth plans—so scaling up feels like a natural next step, not a factory overhaul.
Batching Systems That Hold Your Energy Blend Steady at Any Speed
Mixing energy powders or pellets at changing line speeds often creates invisible drift—start slow and the blend tilts one way, ramp up and it leans the other. This batching system counters that by tying every ingredient feeder to a live weight signal. When the conveyor accelerates, the control loop recalculates dose timing in milliseconds, so each batch still lands within a few grams of the target ratio.
The heart of the setup is a ring of load cells under the mixing chamber, paired with a small industrial controller running a predictive trim routine. Instead of reacting after the mix drifts, it watches the rate-of-change from the previous three batches and nudges auger speed before the imbalance shows up. That keeps the energy blend—whether it is coal dust, biomass, or a custom fuel pellet—steady from a crawl of 5 tons per hour up to a full sprint at 40.
Operators notice the difference mostly in what they stop doing: no more hand sampling every half hour, no more adjusting gate positions by feel, no more rejected batches because the burn test came back hot or cold. The system logs every batch’s actual component weights, so you can pull up yesterday’s run and see the same energy density from the first ton to the last, regardless of how fast the line was moving.
Filling Stations Built for Both Still and Nitrogen-Charged Cans
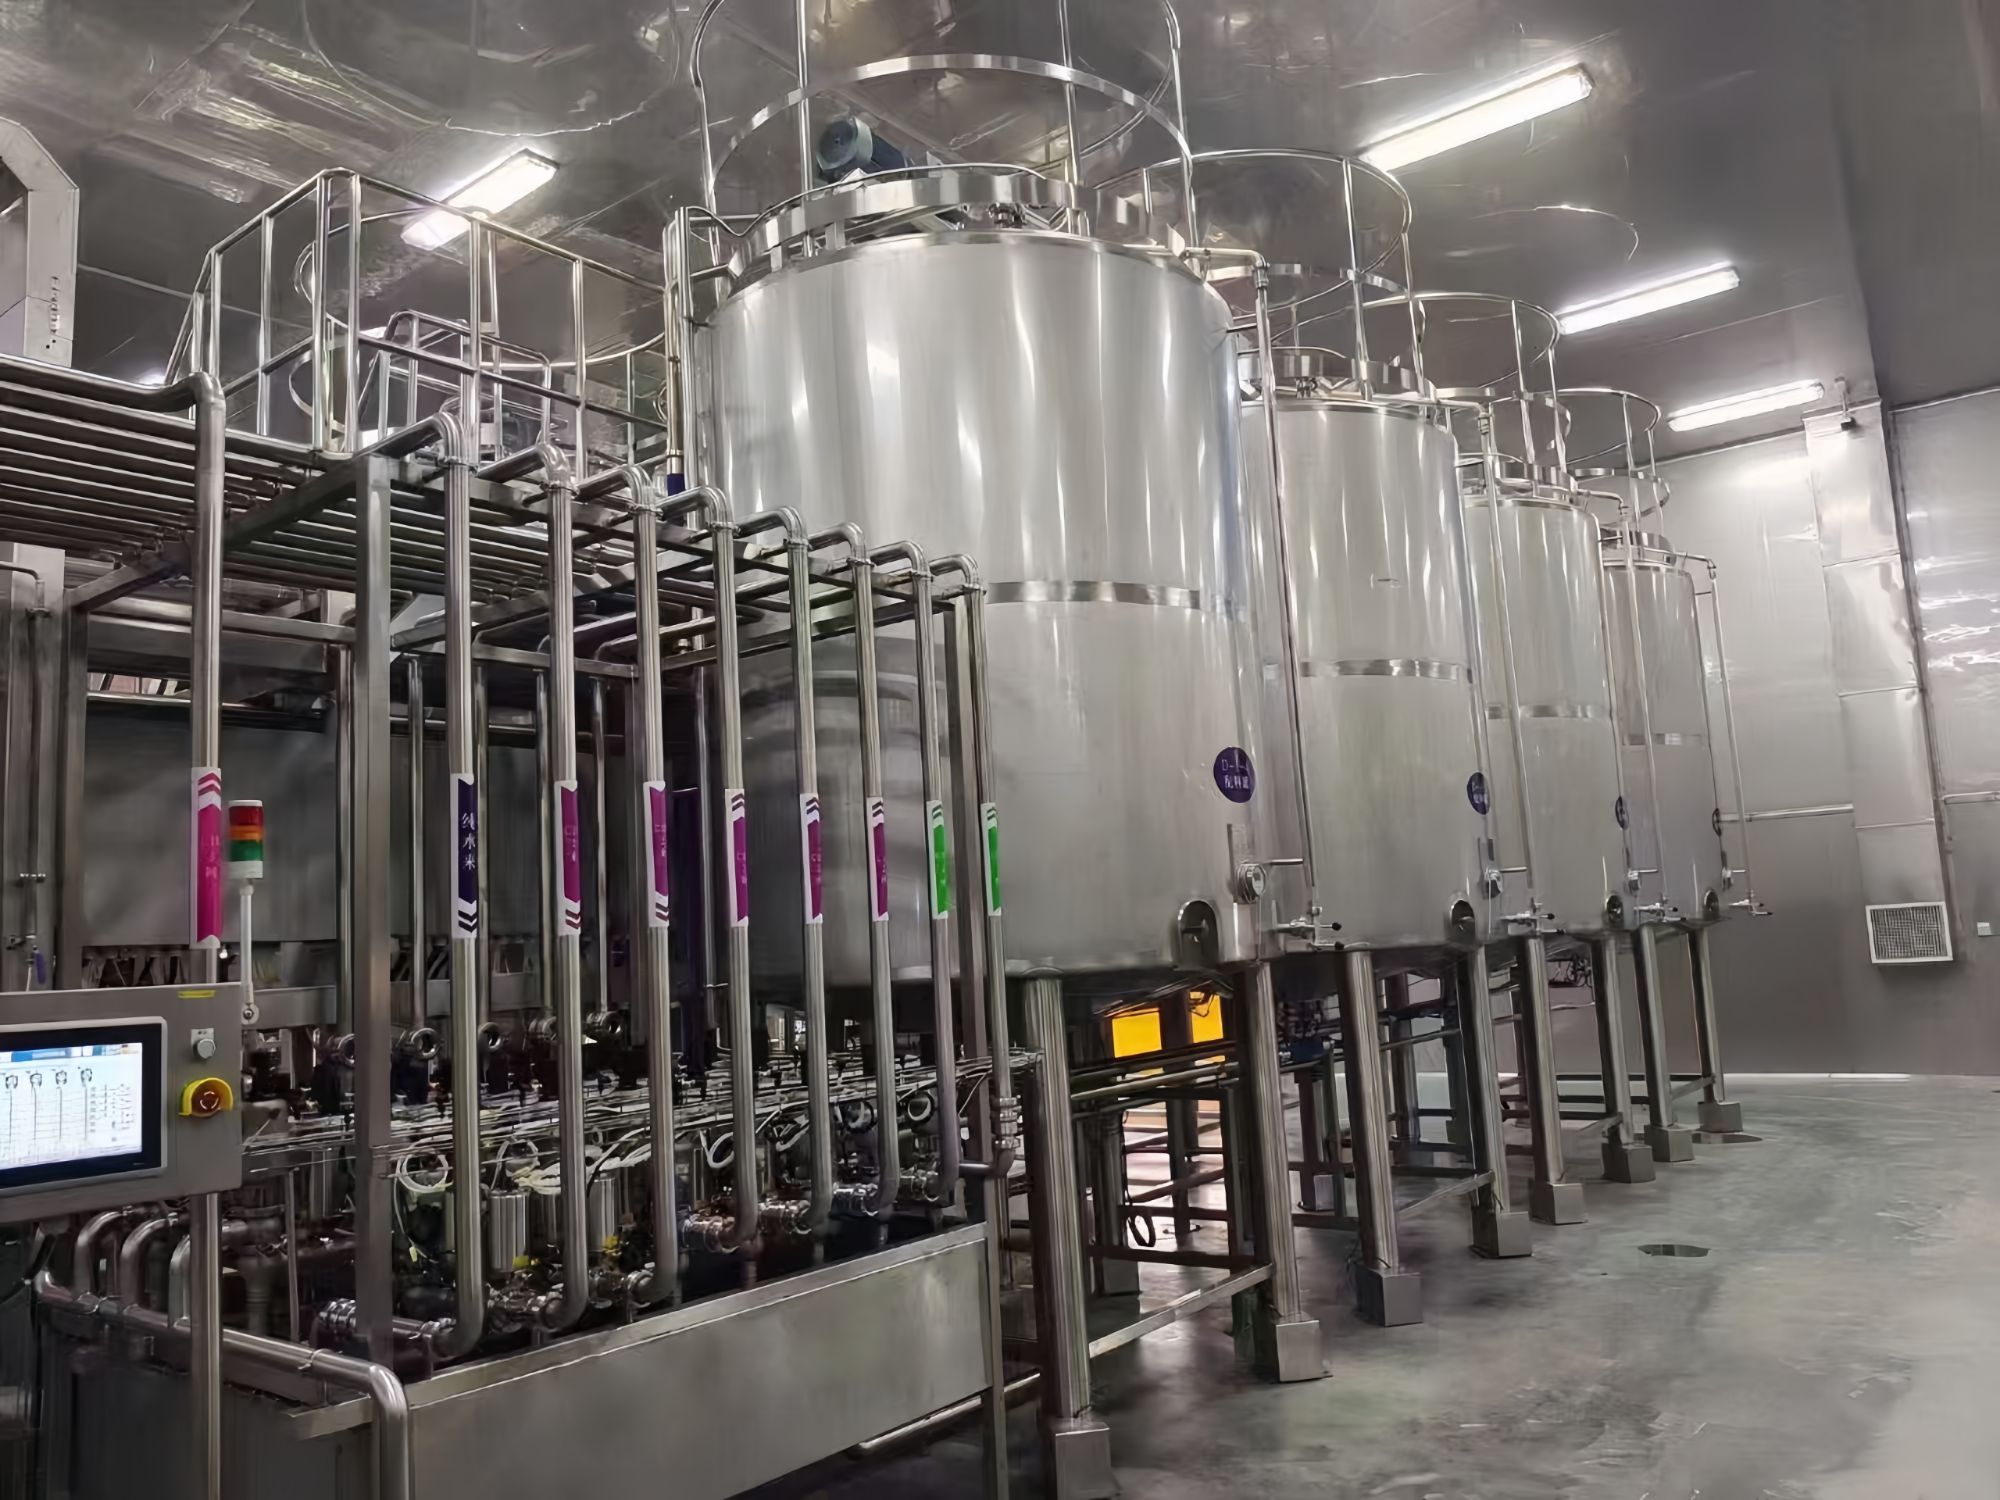
Running two separate canning lines for still and nitrogen-dosed products used to be the norm, but modern filling stations are erasing that divide. These dual-purpose systems let you switch from a cold brew coffee to a nitro stout without swapping out the entire filler head or rewiring the line. The key is a modular gas injection stage that adds a precise burst of liquid nitrogen just before seaming, while the still mode bypasses that step entirely. Operators can toggle between modes from a single control panel, dropping changeover time from hours to under twenty minutes.
What makes these stations stand out is their ability to hold consistent pressure and temperature across both can types. Nitrogen-charged cans demand a higher internal pressure to deliver that signature cascade and tight foam head, whereas still products need a gentler fill to avoid oxygen pickup or excessive foaming. A well-built hybrid station uses independent pressure sensors and flow meters for each lane, so a nitro can gets 30–40 psi of headspace pressure while a still can settles at atmospheric levels. This precision prevents the common headache of cans bulging on the shelf or losing carbonation days after packaging.
Beyond the hardware, the real advantage is flexibility for small and mid-sized producers. Instead of dedicating floor space to two separate machines, a single hybrid filling station handles seasonal releases, limited runs, and contract packaging without locking you into one format. Some units even include a built-in nitrogen generator that pulls gas from the air, cutting supply chain costs and letting you experiment with nitro versions of teas, juices, or even still water on a whim. The learning curve is minimal because the interface uses the same fill, purge, and seam steps—only the dose setting changes.
Automated CIP That Cuts Sanitation Downtime to Minutes
Traditional sanitation often means shutting down lines for manual washdowns that eat hours and depend on operator judgment. This automated CIP system flips that by pre-mapping every pipe, tank, and nozzle, then running targeted rinse, chemical, and sanitize cycles without opening the equipment. The full cleaning sequence finishes in minutes, not shifts.
What sets it apart is the inline sensing and adaptive control. Instead of a fixed timer, the system checks conductivity, temperature, and flow in real time, so each phase ends as soon as residues clear. That prevents over-washing, saves water and chemicals, and creates a verifiable record for every production run without waiting on lab swabs.
For plant teams, this means faster changeovers between products and far less time spent in confined spaces with cleaning chemicals. One operator can trigger the cycle from a mobile panel and move on to other tasks. The equipment comes back ready for production while documentation is already logged.
Changeover Kits That Swap Flavors Without a Wrench
Switching flavors mid-shift used to mean grabbing a set of Allen keys, loosening bolts, and hoping you didn't lose a washer in the drip tray. The new generation of changeover kits eliminates that routine entirely. Each component clicks into place with a satisfying snap, letting you go from blue raspberry to sour apple without ever touching a tool. The flavor modules are keyed and color-coded, so there's no guessing which gasket lines up where—just pull the old block, push in the new one, and you're back to pouring in under thirty seconds.
What makes these wrench-free kits stand out is their sealed interface. Instead of threaded fittings that wear down after repeated swaps, the connection uses a spring-loaded collar that locks the flavor cartridge against a silicone diaphragm. That means no cross-threading, no overtightening, and no slow drips from a misaligned seal. You can even hear a distinct click when the cartridge is fully seated, which takes the guesswork out of installation for new staff. For shops that rotate three or four flavors daily, the time saved adds up fast—and the flavor lines stay pristine because there's no residue left behind from previous syrups.
Beyond convenience, the best changeover kits also rethink the physical layout. Instead of a fixed manifold, they use modular rails that let you slide flavor stations in and out like drawers. This means you can prep extra cartridges in advance, label them with dry-erase markers, and keep a backup lineup in the fridge. When a rush hits, you simply swap the whole rail without breaking down the pump or recalibrating the flow. It's a small shift in design that removes the friction from experimentation—suddenly, offering a limited-time flavor or testing a seasonal blend doesn't require a service call. The wrench stays in the toolbox, and the only thing changing is what's inside the cup.
Throughput That Scales From Test Kitchen to Co-Packer
Bench-scale trials only matter if they survive contact with a real production line. The equipment we use for early runs is deliberately matched to co-packer specifications, so variables like shear rate, residence time, and fill temperature don't drift when volumes jump from 40 liters to 4,000.
Scaling a formula is less about multiplying ingredients and more about understanding where a process bends. We test at throughputs that mimic continuous mixing and inline homogenization, not just a benchtop mixer, because that's where emulsions break and viscosity shifts show up. Fixing those early means the first commercial batch behaves like the hundredth.
Every batch sheet that leaves the test kitchen includes co-packer-ready parameters: target viscosity at transfer, hold time windows, and acceptable deviation at each stage. That documentation turns a recipe into a repeatable process, so a co-packer can run it without guesswork or a long ramp-up.
Live Sensors That Catch Carbonation Drift Mid-Run
Inline CO2 sensors give production teams a live read on carbonation instead of a delayed lab result. When filler speed changes or incoming water temperature shifts, the dissolved gas level can start to slide outside the target band. A fast-responding probe mounted right after the carbonator or in the filler bowl tracks this drift every few seconds. Operators see the trend on a control screen and can make a small setpoint adjustment before the run goes off-spec.
The real payoff comes from closing the loop. A controller can take the sensor's signal and automatically trim CO2 injection pressure or gas flow. If carbonation starts dipping, the system adds a little more gas; if it climbs too high, it backs off. That mid-run correction prevents the waste of filling thousands of bottles or cans that would later be rejected by QA. Some plants also log the sensor data to spot recurring drift patterns tied to specific filler heads or seasonal water supply changes.
FAQ
It usually covers blending and carbonation units, precision filling, capping, labeling, and end-of-line packaging, all configured to match a brand's specific container formats and output targets.
Many systems are built with modular stations, so brands can start with a compact setup and add capacity or new packaging options as demand grows without replacing the whole line.
Yes, through programmable recipes and clean-in-place cycles, the equipment can switch between sugar-free, caffeinated, vitamin-fortified, or sparkling variants with minimal downtime.
Automation handles dosing, filling, inspection, and packaging with consistent accuracy, reducing manual errors and helping brands maintain tight batch-to-batch consistency as they scale.
They allow for unique container shapes, shrink-sleeve or pressure-sensitive labeling, multi-pack formats, and quick changeovers, so brands can launch limited editions or redesigns without long delays.
Inline sensors check fill levels, cap torque, label placement, and carbonation pressure, while automated rejection removes any unit that falls outside set tolerances before it reaches the warehouse.
Modern lines often include low-energy motors, water-saving rinsing systems, lightweight container handling, and recyclable material compatibility, helping brands reduce their environmental footprint while keeping operating costs down.
Key factors include current and projected volume, container type, product viscosity and carbonation level, available floor space, operator training needs, and how easily the line can adapt to future product extensions.
Conclusion
Modern energy drink brands need production lines that don't just keep pace—they adapt. The batching system holds even the most finicky blends steady whether you're running at a crawl or full sprint, so the first can tastes exactly like the ten-thousandth. Filling stations handle both still and nitrogen-charged cans without swapping major hardware, giving you the freedom to switch between a classic crisp finish and that dense, cascading mouthfeel. Automated CIP cycles cut sanitation downtime from hours to minutes, meaning more uptime and fewer late nights for your crew. Changeover kits snap into place without tools, so moving from citrus to berry is a quick handoff rather than a maintenance project.
What really sets this line apart is how it grows with you. Whether you're running test batches in a small kitchen or pushing pallets for a co-packer, throughput scales without a costly rebuild. Live sensors watch carbonation levels in real time and catch drift mid-run, so you can correct a flat batch before it becomes a recall. That kind of visibility turns a typical production shift into a controlled, predictable process—one where your energy blend stays true, your line keeps moving, and your brand can finally focus on the next flavor instead of babysitting the machinery.
Contact Us
Contact Person: Laura
Email: [email protected]
Tel/WhatsApp: +86 13957758832
Website: https://www.intopmachinery.com